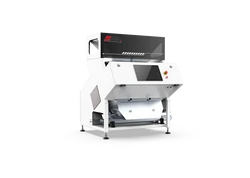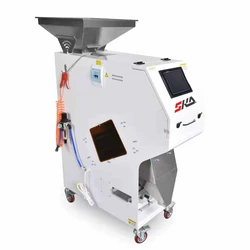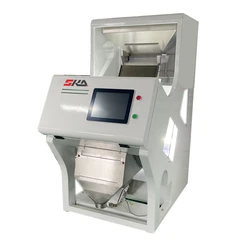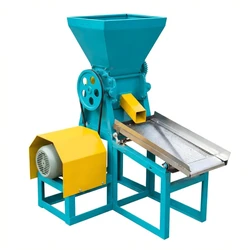


Our coffee color sorting equipment utilizes cutting-edge optical technology and AI algorithms to achieve up to 99.9% sorting accuracy on standard test material, ensuring consistent coffee bean quality while maximizing your production efficiency. Real figures depend on your beans and are confirmed by sample test before you order.
Serving coffee processors, exporters and roasters in 50+ countries
Providing professional color sorting solutions for different industries, customizing the most suitable equipment configuration according to your material characteristics, processing technology and production capacity requirements.
Our coffee color sorting equipment is specially designed for the coffee industry, capable of precisely identifying and removing discolored beans, defective beans, moldy beans, and impurities, ensuring consistency and purity of coffee quality. Using advanced optical technology and AI algorithms, even subtle color differences can be accurately identified, helping coffee producers enhance product quality and meet the strict standards of the high-end coffee market.
We are a global leader in the design and manufacturing of coffee color sorting processing machinery and equipment. With years of experience focusing on the coffee industry, we provide precise, efficient, and reliable color sorting solutions for coffee producers.
Our team of engineers continuously innovates, combining cutting-edge optical technology, AI algorithms with robust mechanical design to develop color sorting processing equipment specifically designed for coffee bean characteristics, meeting the increasingly demanding quality requirements of the coffee industry.
We provide comprehensive services from single equipment to complete factory solutions, including equipment installation, personnel training, and after-sales support, ensuring your coffee processing production line operates efficiently and stably.

Explore the innovative technologies of our coffee color sorting processing equipment and understand why we are the best choice for coffee producers.
Throughput from 30 kg per hour to 2.5 tons per hour, confirmed on your material before you order.
Advanced optical sensors and AI algorithms (on AI-equipped models) reach up to 99.9% accuracy on standard test material. Your actual rate is measured in a sample test.
On AI-equipped models, machine learning algorithms adapt to different coffee lots and keep improving recognition over time.
Low power consumption design helps reduce operational costs and environmental impact.
Advanced software provides detailed analytics and performance monitoring.
User-friendly design allows for quick cleaning and minimal downtime.
Control and monitor your sorting machine from anywhere using our mobile app.
Tailor the sorting parameters to your specific product and quality requirements.
Certification, sample-tested configuration and after-sales support — the same standard across the whole hulling, sorting and roasting line.
Learn how our coffee color sorting processing equipment helps coffee producers worldwide improve quality, increase efficiency, and achieve business growth.
An advanced coffee defect removal system designed for exporters and processing mills. Learn how high-precision optical sorting stabilizes coffee batch quality, eliminates severe defects, and secures premium export market pricing.
View Details
An advanced green coffee bean sorting solution designed for exporters and processing mills. Learn how automated optical sorting removes severe color defects, stabilizes batch quality, and helps you achieve export-grade standards.
View Details
An advanced roasted coffee bean color sorting solution designed for specialty roasters and packaging facilities. Learn how high-precision optical recognition detects roast defects and stabilizes your product appearance.
View DetailsSuccess Stories
Countries Covered
Years Export Experience
Global Customers
What a coffee color sorter warranty really covers, what it leaves out, and which service terms belong in writing before you buy. Includes SKA's actual coverage.
Read More
Ten color sorter manufacturers compared on coffee fit, sensor tech and service reach, plus where SKA Machinery fits for small and mid-size processors.
Read More
Compare small and industrial coffee color sorters on throughput, power, footprint and downtime cost, then match the right class to your daily volume.
Read MoreContact us now to schedule a demonstration and learn how our coffee color sorting processing equipment can help you improve coffee quality, increase production efficiency, and reduce costs.